• Welcome to ClassicBroncos! - You are currently viewing the forums as a GUEST. To take advantage of all the site features, please take a moment to register. It's fast, simple and absolutely free. So please join our community today!
    If you have problems registering or can't log into your account, please contact Admin.

Welding Help

Tulsa76bronco

Sr. Member
Joined
Apr 23, 2013
Messages
635
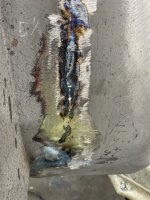
Welding blow through. I welded the wheel well back on but when fringing it flat noticed some thin areas that looked cracked, basically ground down too much trying to smooth it out. Lesson learned.
Now when I tried to quickly put a weld a bead on each side to bridge it just blew through. How do I weld this with wheel well so thin.
 

Attachments

  • IMG_3866.jpeg
    IMG_3866.jpeg
    342.5 KB · Views: 104
  • IMG_3867.jpeg
    IMG_3867.jpeg
    246.5 KB · Views: 91
  • IMG_3865.jpeg
    IMG_3865.jpeg
    268.6 KB · Views: 111
  • IMG_3288.jpeg
    IMG_3288.jpeg
    202.2 KB · Views: 111
  • IMG_3289.jpeg
    IMG_3289.jpeg
    289.1 KB · Views: 115
  • IMG_3290.jpeg
    IMG_3290.jpeg
    280.5 KB · Views: 100

rocknhorse76

Contributor
Bronco owner since 1993 💪🏻
Joined
Jun 7, 2014
Messages
463
Loc.
Central WA
I use a fairly thick piece of copper plate on the backside of the material and .023” wire. Keep the heat low and don’t dwell in one spot too long.
 

gnpenning

Contributor
Bronco Slave
Joined
Dec 26, 2011
Messages
2,598
Loc.
I have more questions than answers.
To expand on the previous replies.
If you have a short piece of copper pipe, hammer it flat, or split it and hammer flat. Bend to any angle you need and form a handle as needed. Same if you have a piece of aluminum.

Might be easier than buying one depending on what you have on hand.
 

ntsqd

heratic car camper
Joined
Jan 30, 2005
Messages
5,953
Loc.
Upper SoKA
On top of all of the suggestions, and sometimes instead of them I'll 'doodle' a gap like that. Think of successive spot welds, with a 5 to 10 count between each of them. You don't want to merely wait for the red to go out of them, you need them cooler than that.

It helps me to think of welding as being an "on-site casting process".
 

jeffncs

Contributor
Bronco Guru
Joined
May 4, 2004
Messages
1,894
Loc.
Raleigh, NC
You can’t typically run a weld bead on sheet metal without warping the panel or blowing it out. Think of it as a series of 1000 spot welds.

Looking at the pics - your welds look cold which means you’re likely spending too long to build up a bead…which then blows out the thinner metal.

Bump the heat up a notch (typically 3 on the scale of 5) and set the wire speed to 25-30. Listen to your machine - it’ll tell you more/less heat and more/less wire based on a neat little buzz.

Keeping the old-new metal gap to about 1/16”, Angle the wire at ~30° to the surface aiming at the side with the thicker metal.

It takes a lot of practice and time to get it right but it can be done. I promise!
 
Top